Follow #GEODRYTECH


A Chemical Reactor is a critical processing container, in which controlled chemical reactions are performed safely and efficiently. Popular applications include mixing, heating and cooling, blending and chemical reactions for the pharmaceutical, API, chemical, food and specialty chemical industries.
In Geo Drytech, we design, manufacture and sell high-performance, reliable, excellent heat transfer, consistent product quality industrial chemical reactors. With a long history of providing trusted custom chemical reactor manufacturers, we supply 1 KL chemical reactors, 5 KL chemical reactors as well as bigger capacities to suit a variety of manufacturing needs.
The chemical reaction systems are available in stainless steel SS304 and SS316 construction materials, which have good corrosion resistance and long use life. We also produce jacketed chemical reactors that are equipped with efficient heating and cooling mechanisms to ensure a precise temperature during critical processing stages.
For regulated industries, our GMP chemical reactors are built with hygienic designs that comply with stringent quality standards. From Fine Chemicals and Specialty Chemicals to pharmaceutical intermediates and other industrial products, our reactors provide safe, efficient and reliable operation and reduce your maintenance time and increase your productivity.
| Model No. | Total Capacity (L) | Working Capacity (L) | Material of Construction | Heating/ Cooling | Agitator Motor (HP) |
|---|---|---|---|---|---|
| GEO-CR-1 | 1000 | 800 | SS304 / SS316 / SS316L | Jacketed | 3 |
| GEO-CR-2 | 2000 | 1600 | SS304 / SS316 / SS316L | Jacketed | 5 |
| GEO-CR-3 | 3000 | 2400 | SS304 / SS316 / SS316L | Jacketed | 7.5 |
| GEO-CR-5 | 5000 | 4000 | SS304 / SS316 / SS316L | Jacketed | 10 |
| GEO-CR-10 | 10000 | 8000 | SS304 / SS316 / SS316L | Jacketed | 15 |
| GEO-CR-15 | 15000 | 12000 | SS304 / SS316 / SS316L | Jacketed | 20 |
| GEO-CR-20 | 20000 | 16000 | SS304 / SS316 / SS316L | Jacketed | 25 |

The chemical reactor consists of a jacketed reactor to provide even heating and cooling of the batch. It can be used for steam, hot water, thermal oil or chilled water circulation, and can control the reaction temperature accurately to achieve high reaction efficiency, uniform product quality and shorten the reaction time.

The reactor is made of high quality SS304, SS316 or SS316L stainless steel materials, which have good corrosion resistance, chemical resistance and heat resistance. It is well-known that its sturdy construction will last for a long time, have a high reliability and minimal maintenance in harsh industrial environments.

Advanced agitators like anchor, paddle, turbine or propeller types are fitted in the reactor to ensure complete mixing of liquids, powder and viscous material. This will assure the even dispersion, better mass transfer and uniform reaction results throughout the batch.

The reactor is used to maintain reaction conditions during the process, ensuring accurate temperature, pressure and mixing speed control. This will help to maintain product uniformity, increase product yield and decrease the likelihood of process differences.

The GMP Chemical Reactor has smooth inner walls and is crevice-free and easy to clean and maintain. It is hygienic, reducing contamination risks and suitable for pharmaceutical, API, food, and other industries that require high-quality products.

The reactor can be designed in various sizes and materials, including 1 KL Chemical Reactor, 5 KL Chemical Reactor, larger, and custom-built, with options for different agitators, pressure ratings, and heating methods to meet the needs of various processes.

The reactor is designed with quality components and precision manufacturing, which guarantees the safe operation of the reactor under atmospheric, pressure or vacuum conditions. Process reliability is further enhanced by optional process safety equipment like pressure relief valves, temperature sensors and automated controls.

The jacket is optimized in its design to maximize the amount of heat transferred with the minimum amount of energy used, and the mixing system is efficient. This leads to faster batch cycles, lower operating costs and better overall production efficiency.

The reactor has been designed for easy inspection, cleaning and maintenance to minimize down time and maximize operating efficiency. It is made with top quality components and heavy duty construction for guaranteed reliability and value to manufacturers.
Chemical reacts with different industries such as pharmacy, agrochemical, cosmetic, and fine chemical.
The Chemical Reactor is used extensively in industries that require the controlled chemical reaction, good mixing and accurate temperature control. It has a wide application scope and can be used to produce various products, maintain product quality, improve production processes and ensure production reliability.
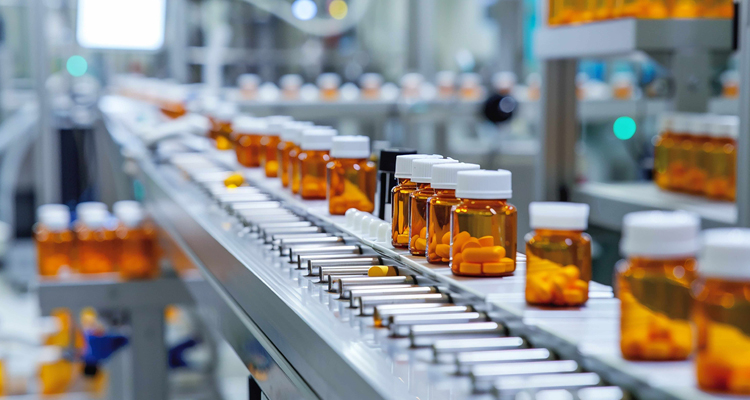
Processed under controlled conditions for the production of pharmaceutical intermediates, pharmaceutical formulations, medicinal syrups and medicinal products, preserving the purity and quality of the product.
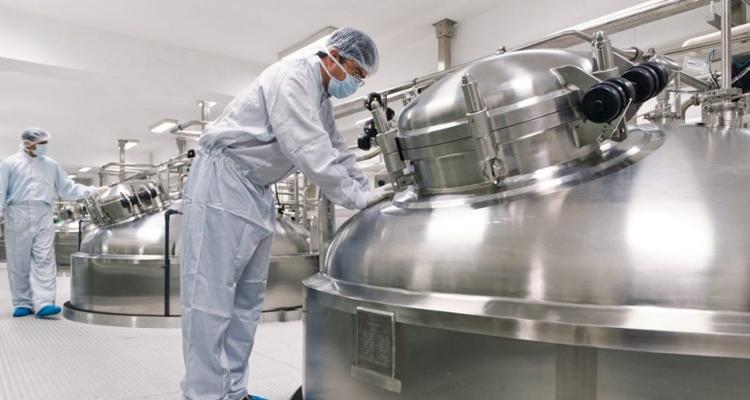
Perfect for Active Pharmaceuticals (APIs) and high value pharmaceuticals that demand a high level of temperature control, mixing and a GMP process.
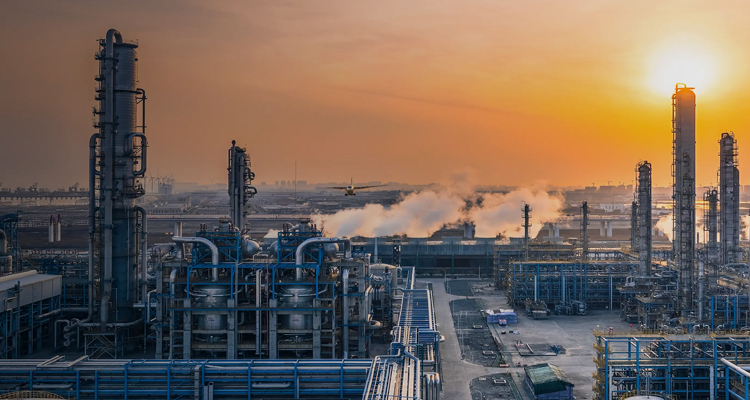
Ideal for processing organic and inorganic chemicals, solvents, acids, alkalis and polymers, industrial chemical formulations with consistent and reliable performance.

For manufacture of high value fine chemicals where accurate reaction control, uniform mixing and consistent product quality are crucial throughout the manufacturing process.

Widely used for specialty chemicals, catalysts, additives, performance chemicals and customized formulations that require specific processing conditions.
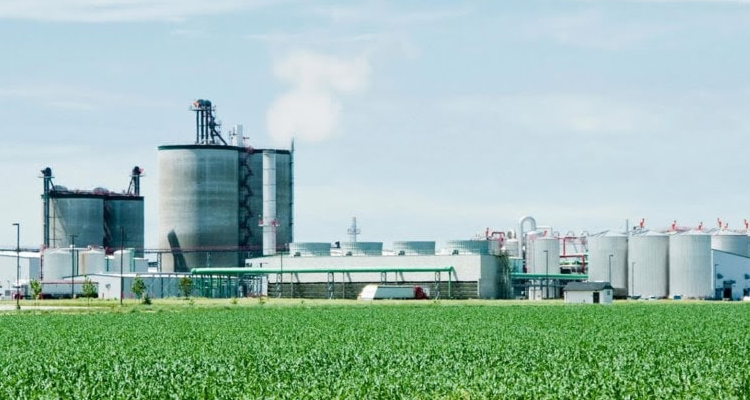
Enables safe, efficient and reliable processing of agrochemical products such as pesticides, herbicides, insecticides, fungicides, fertilizers and so on.
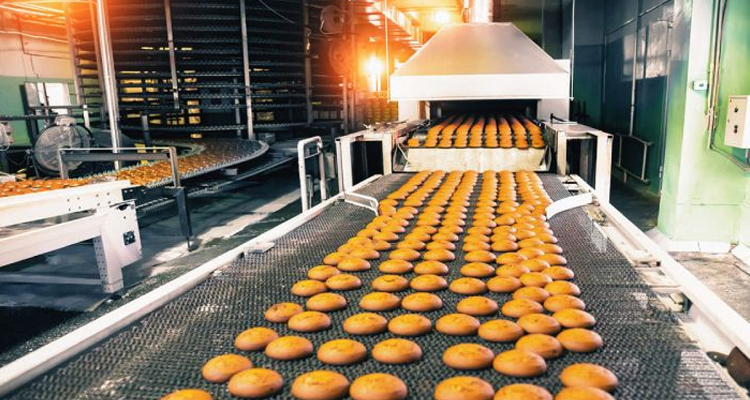
Syrups, flavoring agents, additives, starches and other food grade products are used to prepare food ingredients under hygienic conditions for mixing, heating, blending and processing.
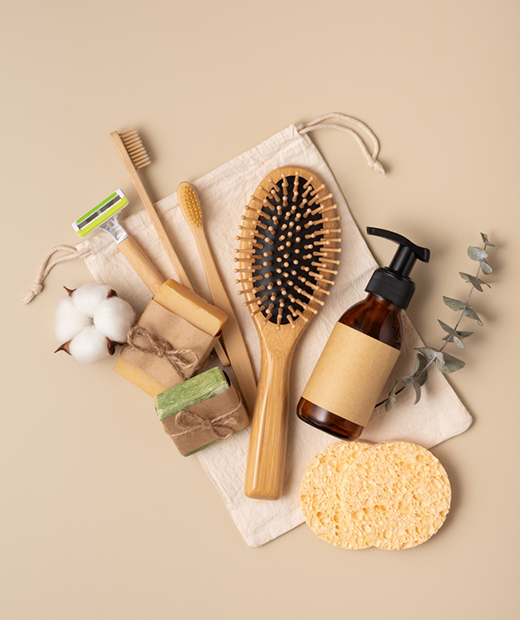
Ideal for mixing uniform creams, lotions, gels, shampoos, liquid soaps, ointments and cosmetic formulations and controlled heating.
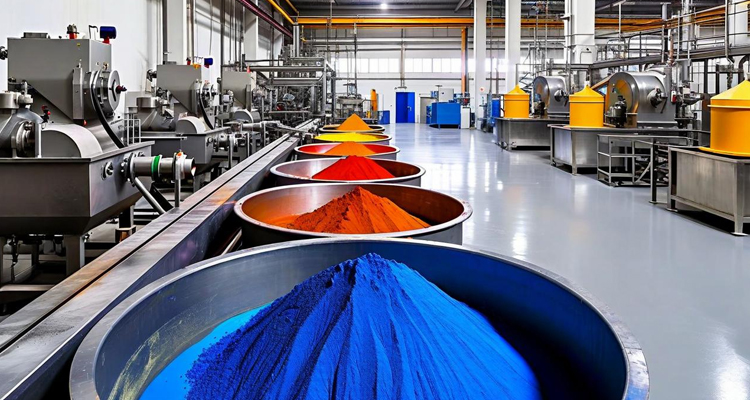
Operates dyes, pigments, colourants, inks and specialty coating materials efficiently and in a manner that provides consistent product quality and batch consistency.

Performs well in the production of adhesives, resins, emulsions, sealants and polymer-based products where controlled chemical reactions and mixing is necessary.
Chemical reactors are widely used to carry out controlled chemical reactions to synthesize both organic and inorganic chemicals. Control over temperature, pressure and mixing is essential for greater reaction efficiency, superior yield and uniformity of product quality.
The reactor is an efficient mixing apparatus for liquids, powder, slurry and viscous substances to obtain homogeneous mixture. Agitators with high performance have no dead zones and can achieve uniform mixing throughout the batch.
Steam, hot water, thermal oil and chilled water can be used for controlled heating and cooling of the reactor, which is furnished with a jacket or limpet coil. This keeps the reaction temperature as it is desired, and avoids product degradation during production.
Chemical reactors play a vital role in manufacturing various polymers, synthetic resins, latex, adhesives and plastic compounds. Consistent polymer properties and product quality are guaranteed by uniform agitation and accurate temperature control.
The reactor is well suited for the production of pharmaceutical formulations, Active Pharmaceutical Ingredients (APIs), intermediates and bulk drugs. The product purity and the high standards for pharmaceutical manufacturing are guaranteed by the GMP compliant construction and hygienic design.
Controlled crystallization of chemical compounds and pharmaceutical products are carried out in chemical reactors. Process stability enables desirable crystal size, purity and uniform particle size distribution for better downstream processing.
The reactor is effective to make stable emulsions and suspensions for pharmaceutical, cosmetic, food and chemical applications. The continuous agitation provides uniform dispersion of ingredients and uniformity of the product.
Ideal for production of synthetic resins, industrial adhesives, sealants, coatings and specialty polymers that require controlled reaction conditions and efficient heat transfer throughout the manufacturing process.
Ideal for processing solvent based formulations and volatile chemicals, in a safe enclosed reactor design. It enables the efficient heating, cooling and even pressure or vacuum operation which improves process safety and quality of the product.
Chemical reactors are widely employed in the manufacture of fine chemicals, specialty chemicals, catalysts, dyes/pigments, performance chemicals and customized formulations, which demand precise process control, uniform mixing and consistent chemical reaction performance.
A chemical reactor is used to ensure the reaction conditions are controlled during the reaction by keeping the reaction temperature, pressure and mixing constant throughout the reaction. This helps to achieve uniform product quality, minimize batch variations and give consistent production each time.
The reactor promotes chemical reactions to be carried out at a faster rate, and enhances the overall process performance by efficient heat transfer, continuous agitation. Fast reaction cycles enable manufacturers to boost productivity while cutting down reaction time.
The jacketed design enables precise heating and/or cooling with steam, thermal oil, hot water or chilled water. Not only will this increase the efficiency of the reaction but it will also help to prevent degradation of heat-sensitive materials.
The agitation system is designed for good mixing of liquids, powders and viscous materials. Reactions are more efficient and a uniform product is more easily obtained due to uniform mixing which results in uniform mass and heat transfer.
Chemical reactors can be used for chemical synthesis, chemical blending, polymerization, crystallization, emulsification and chemical processing of solvents in a single system. This versatility allows it to be used in several industrial applications.
The reactor is made of high quality stainless steel, and the inside surface is smooth, easy to clean and maintain. GMP compliant designs also bolster industries that have a heightened focus on hygiene, product purity and contamination control.
The heating and cooling system is optimized for thermal efficiency with a minimum use of energy. A decrease in energy consumption can result in lower operating costs and greater energy sustainability in production.
Following the elegant design and robust construction, the reactor is designed to work reliably under atmospheric, pressure and vacuum conditions. Other options for safety and automation further improve the safety of the process and reliability of its operation.
Each manufacturing process has its own needs. Chemical reactors are available in various sizes, with different agitators, materials of construction, heating methods and automation systems to suit particular production requirements.
